 info@unicomposite.com


Quick answer
Fiberglass rebar is typically made by combining continuous glass-fiber reinforcement with a polymer matrix, consolidating the composite into a bar, adding a bond-promoting surface, and cutting or shaping it for the project. The reliable way to review a process is to trace material identity, forming controls, dimensional checks, tensile/bond evidence, lot records, and release documents. Ask for records that match the exact bar being specified.
We organize this guide around the records an engineer or buyer can review before approving a bar. The sequence is supplier-neutral: it explains the industry process without presenting it as a description of Unicomposite’s own line.
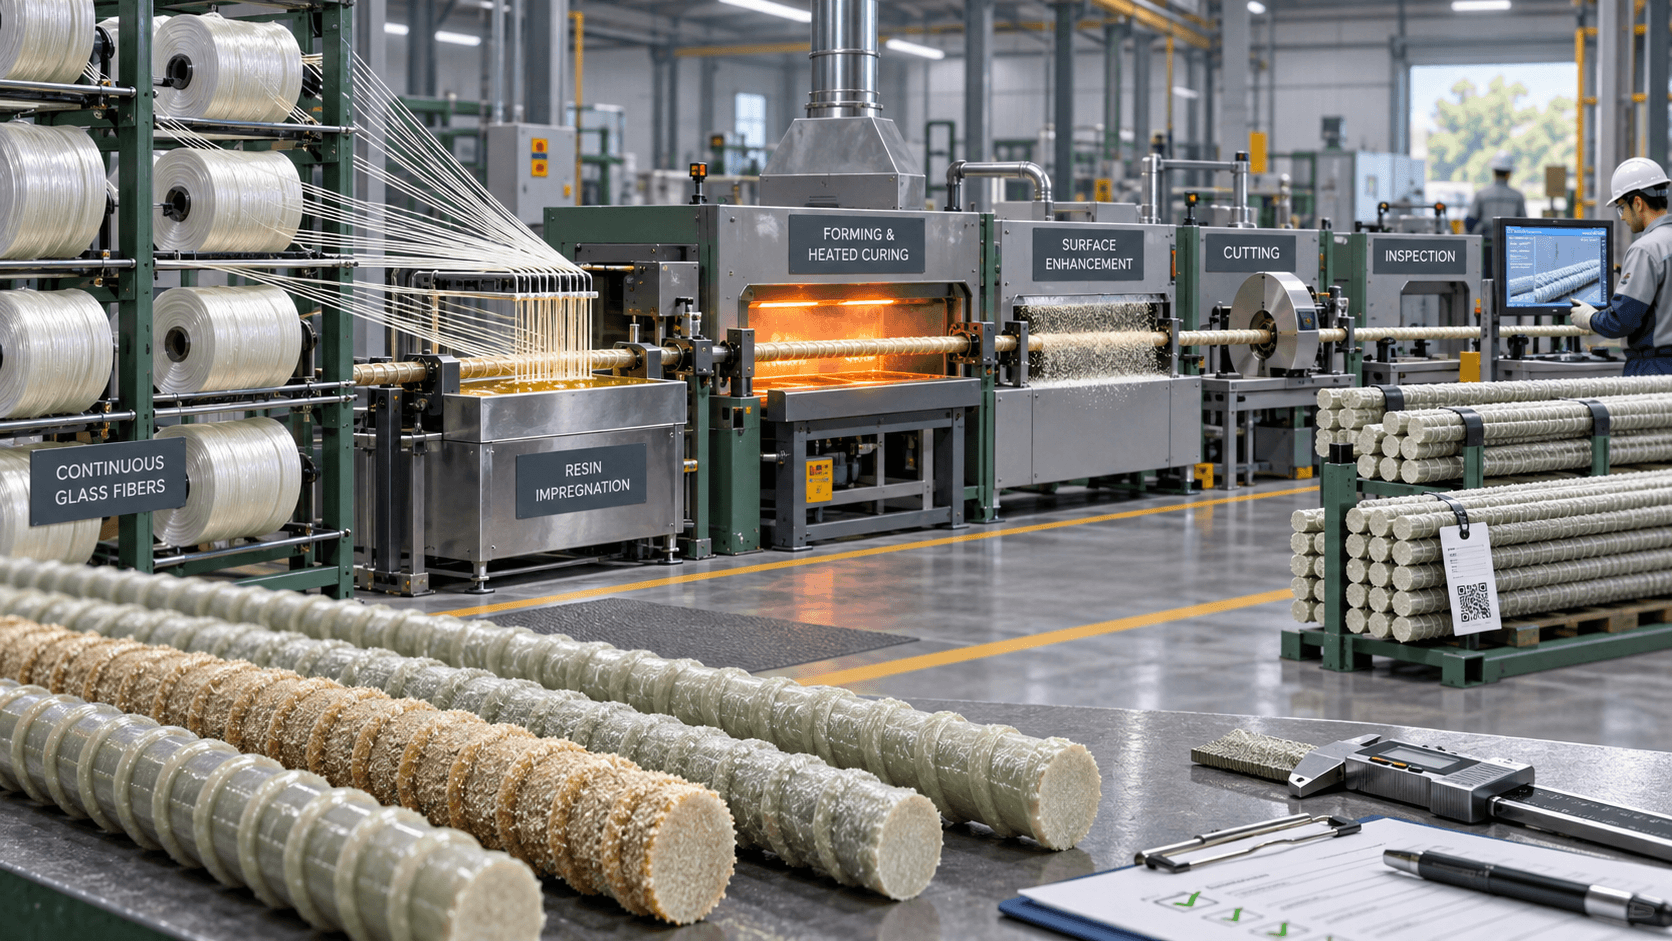
fiberglass rebar manufacturing process
What a fiberglass rebar manufacturing process must deliver
“Fiberglass rebar” is a market term for glass-fiber-reinforced polymer (GFRP) reinforcement. We use four outputs to keep a process description actionable:
- A defined material system. The reinforcement, resin matrix, additives and any surface materials must be identified at the level required by the project.
- A consolidated bar. Fibers need to remain aligned and sufficiently impregnated while the matrix is formed and cured.
- A concrete-bonding surface. The exterior geometry or treatment transfers force between the bar and the surrounding concrete.
- Reviewable records. A buyer needs a controlled specification, test basis, lot identity and release documentation—not only a photograph of equipment.
ASTM D7957/D7957M-26 describes GFRP bars as cut lengths or bent shapes with an external surface enhancement and separates qualification from quality control and production-lot acceptance. That distinction is the foundation for the process review below.
Materials Used in Fiberglass Rebar Manufacturing
The material system normally has three functional elements:
- Glass-fiber reinforcement: continuous fibers provide the longitudinal reinforcement within the composite bar. The exact fiber type, arrangement and grade are product-specific.
- Resin matrix: the polymer binds and protects the fibers while transferring stress through the composite. Resin chemistry and cure requirements must be identified in the controlled product documentation.
- Surface-enhancement system: a textured, wrapped, ribbed, sanded or otherwise formed exterior transfers force between the bar and the surrounding concrete.
These categories explain the industry material architecture; they are not a Unicomposite grade or a product specification. Confirm the actual fiber, resin, surface design and qualification basis for the bar being ordered.
The six stages of an industry process
1. Define and receive the incoming materials
The process starts before the first fiber enters a forming line. The purchaser and producer should agree on the fiber type, resin system, surface materials, identification format and storage conditions. Incoming records should connect each material container or spool to a lot number, supplier document and release decision.
Do not fill gaps with an “industry-standard” resin or fiber grade. A generic GFRP label does not identify the actual chemistry, fiber arrangement or qualification basis of a particular bar. If the material identity is not controlled, later test results cannot be confidently tied to the delivered product.
Useful evidence: approved material list, supplier certificate or batch record, receiving inspection, storage log and nonconformance disposition.
2. Feed the fibers and achieve resin wet-out
In a representative pultrusion route, continuous glass filaments are drawn through a resin bath and then through a forming die. The Federal Highway Administration describes this sequence for GFRP dowels; it is a helpful industry model, not a claim that every rebar uses the same equipment or resin. See the FHWA description of pultruded GFRP elements.
At this stage, the process must control fiber tension, alignment, resin proportioning, wet-out and the removal of voids or dry areas. The important question is not whether a supplier uses the word “pultrusion,” but whether the supplier can show how those variables are monitored and what happens when a signal leaves its approved range.
Useful evidence: work instruction revision, line-start checklist, resin-batch linkage, in-process observations, alarm or hold records and corrective-action records.
3. Form, consolidate and cure the bar
The impregnated fiber bundle is shaped to the required cross-section and cured into a stable composite. Die geometry, heat profile, pull speed, cure state and line changes can affect consolidation and dimensional consistency. Exact setpoints are product- and equipment-specific; they should come from the controlled process specification rather than from a general article.
The output of this stage is a continuous or discrete bar with a defined cross-section and a documented process state. A supplier should be able to distinguish qualification data from routine production data and explain which changes require requalification.
Useful evidence: approved process window, equipment identification, calibration status, cure or degree-of-cure record where required, start/stop traceability and change-control record.
4. Create and verify the concrete-bonding surface
The outer surface may be textured, wrapped, ribbed, sanded or otherwise formed. It is not merely cosmetic: it changes how force is transferred into concrete. ASTM D7957 includes an external surface enhancement within its scope, while ASTM D7913/D7913M-26 provides a standardized pullout method for evaluating bar-to-concrete bond.
Pullout data still needs careful interpretation. ASTM notes that the pullout configuration should not by itself establish design bond values or development lengths. Those decisions belong to the governing design provisions and the responsible design professional.
Useful evidence: surface specification, surface-process inspection, visual acceptance criteria, dimensional checks and bond-test records linked to the same product identity.
5. Cut, shape, mark and protect the finished bars
After forming and surface treatment, bars are cut to scheduled lengths or supplied as qualified bent shapes where the product and specification allow them. ASTM D7957 explicitly distinguishes cut lengths and bent shapes, so a straight-bar result should not automatically be used to approve a bent product.
Marking and packaging complete the identity chain. Each bundle or shipment should retain the product designation, lot, length or shape information, handling instructions and the document revision used for release. Damaged surfaces, mixed lots or unreadable marks should trigger a hold rather than an assumption that the material is acceptable.
Useful evidence: cutting or shaping record, final visual inspection, bundle label, packing list, damage report and release authorization.
6. Release the production lot with the right tests
Qualification demonstrates that a product design and process can meet the applicable requirements. Production-lot acceptance demonstrates that the lot being shipped remains within those requirements. ASTM D7957 separates these activities and points to test methods for mechanical and physical properties.
The test list should follow the project specification and exposure. Common evidence routes include:
- Tensile properties: ASTM D7205/D7205M for the tensile test method used to report force, strength, strain and modulus-related results.
- Transverse shear: ASTM D7617/D7617M-25, which describes a double-shear method used for material specifications, quality control and quality assurance.
- Bond behavior: ASTM D7913/D7913M-26, interpreted as a specimen-configuration-dependent result rather than a stand-alone development-length value.
- Alkali exposure: ASTM D7705/D7705M-26, where the exposure, sustained stress condition and post-conditioning tensile test must be reported.
- Sustained-load risk: ASTM D7337/D7337M-26 for tensile creep-rupture data when sustained loading is relevant to the design.
The release package should state the exact standard edition, specimen basis, sampling plan, result statistic, acceptance rule and lot number. A certificate that names a standard without connecting it to the supplied bar is not enough for approval.
A practical quality-control evidence chain
| Process point | Engineering signal | Verification output | Decision condition |
|---|---|---|---|
| Incoming materials | Identity, lot, condition and storage | Receiving record and material release | Hold if identity or condition is unresolved |
| Fiber/resin feed | Tension, proportioning, wet-out and line status | In-process checklist and deviation log | Continue only inside the approved process window |
| Forming and cure | Cross-section, consolidation and cure state | Process record and calibration status | Stop or segregate when a critical variable drifts |
| Surface enhancement | Geometry, coverage, adhesion or texture | Visual/dimensional record plus applicable bond evidence | Do not release a bar with an unverified surface state |
| Finished bar | Dimensions, appearance, markings and damage | Final inspection and bundle traceability | Rework, segregate or reject against the written rule |
| Production lot | Tensile, shear, bond or durability tests as specified | Test report tied to lot and revision | Release only when every required criterion is met |
This chain also makes audits faster. The reviewer can start from a bundle label, move to the lot record, then follow the material and process records back to the incoming batches. If any link is missing, record the gap instead of substituting a value from another bar or another manufacturer.
Questions to ask when reviewing a supplier’s process
When preparing a technical inquiry or pre-award review, use these questions:
- What fiber type, resin system and surface configuration are identified for the exact bar?
- Which standard and edition define qualification, production-lot acceptance and test methods?
- Which process variables are critical, and what is the approved operating window for them?
- How are fiber, resin and surface-material lots linked to the finished bundle?
- Which dimensions and surface features are inspected, with what sampling frequency and acceptance rule?
- Which results are qualification values, which are lot results, and how are averages or guaranteed values defined?
- Are tensile, shear, bond, alkali or creep tests required by the project, and do the reports use the requested methods?
- How are nonconforming bars identified, isolated, investigated and dispositioned?
- What changes to materials, die, surface treatment or cure require customer notification or requalification?
- Can the supplier provide a controlled submittal pack that matches the bar schedule, shape, destination and governing design provisions?
For procurement sequencing, see our contractor buying guide for fiberglass rebar suppliers. Use it as a document-planning aid and verify every commercial or technical statement against the current project submittal.
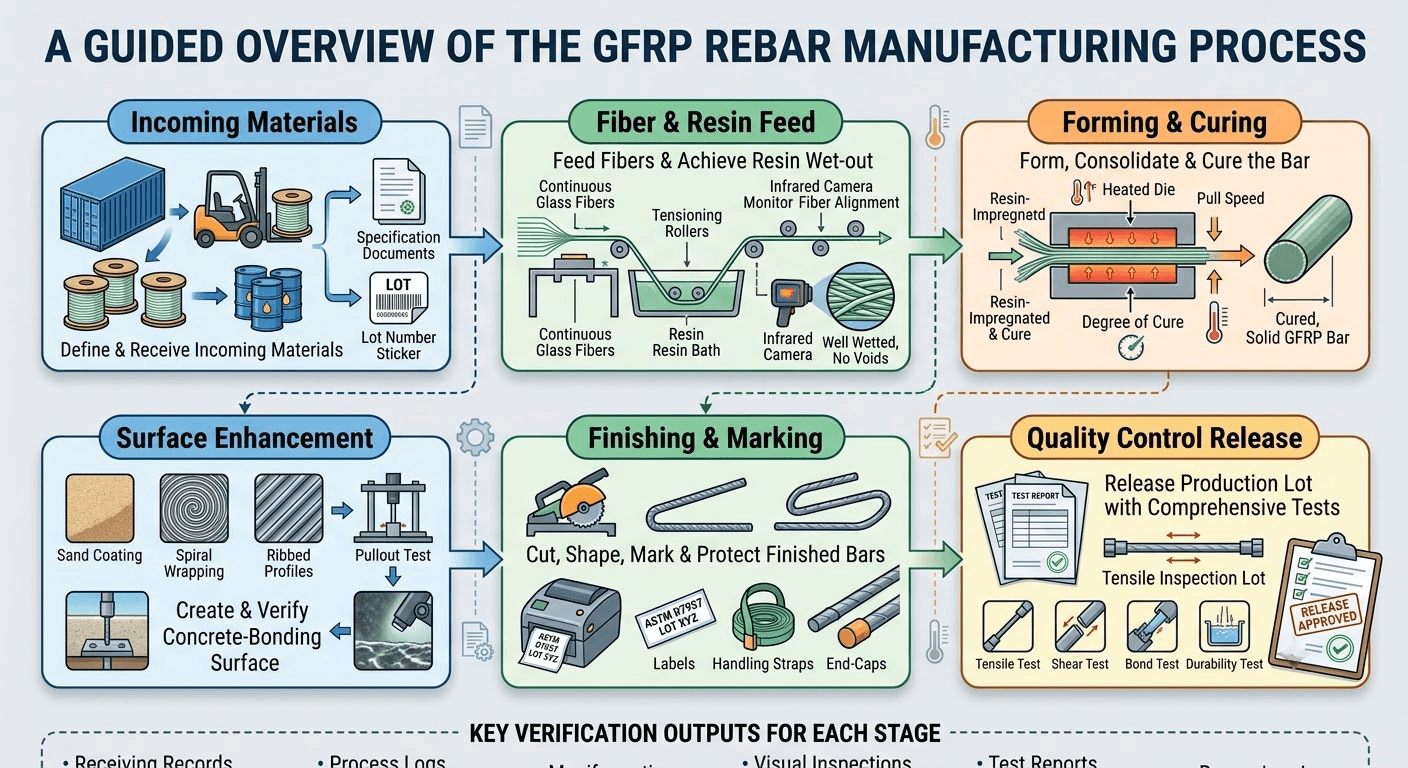
a guided overview of the gfrp rebar manufacturing process
What a process description does not prove
The following shortcuts create avoidable approval risk:
- “Advanced equipment” is not a test result. A machine photograph does not establish wet-out, cure or dimensional control.
- A process name is not compliance. “Pultruded” does not identify the standard edition, product scope or lot acceptance record.
- One successful specimen is not production consistency. Qualification, routine lot testing and traceability answer different questions.
- A bond result is not automatically a design length. Use the governing code and the responsible engineer’s detailing review.
- A standard logo is not a certificate. Check the product identity, test method, report date, sample basis and approval status.
- Rebar and rock bolt records must stay separate. Similar composite terminology does not make the products interchangeable.
Connect the process review to the concrete design
Manufacturing evidence is only one part of approval. ACI CODE-440.11-22 addresses structural concrete reinforced with GFRP bars and covers design and construction topics such as strength, serviceability, durability, development, splicing, inspection and testing. The project team must name the governing code and edition, confirm the bar identity and use the applicable design provisions.
For terminology and a broader specification framework, see our GFRP rebar terminology, composition and applications guide. A diameter or a generic “fiberglass rebar” label is not a complete project specification.
Once the manufacturing evidence requirements are clear, the next step is to match the project specification with an appropriate product scope.
Our FRP rebar project scope
Our FRP rebar offering is a fiberglass-and-resin composite for concrete reinforcement, and the page provides a direct inquiry route. Project-specific fiber and resin details, geometry, mechanical properties, applicable specifications, quantities and document availability are confirmed during project discussion and quotation.
If you are preparing an inquiry, send the project location, governing code and edition, structural drawings, bar schedule, required shapes and lengths, quantity, exposure conditions, document requirements, destination and acceptance criteria. We will use those inputs to define the quotation scope and identify the product and document requirements for review.
References
- ASTM D7957/D7957M-26 — Standard Specification for GFRP Bars for Concrete Reinforcement
- ASTM D7205/D7205M-26 — Tensile Properties of FRP Composite Bars
- ASTM D7617/D7617M-25 — Transverse Shear Strength
- ASTM D7913/D7913M-26 — Bond Strength by Pullout Testing
- ASTM D7705/D7705M-26 — Alkali Resistance
- ASTM D7337/D7337M-26 — Tensile Creep Rupture
- ACI CODE-440.11-22
- FHWA — Representative pultruded GFRP element process


