 info@unicomposite.com


Quick Answer
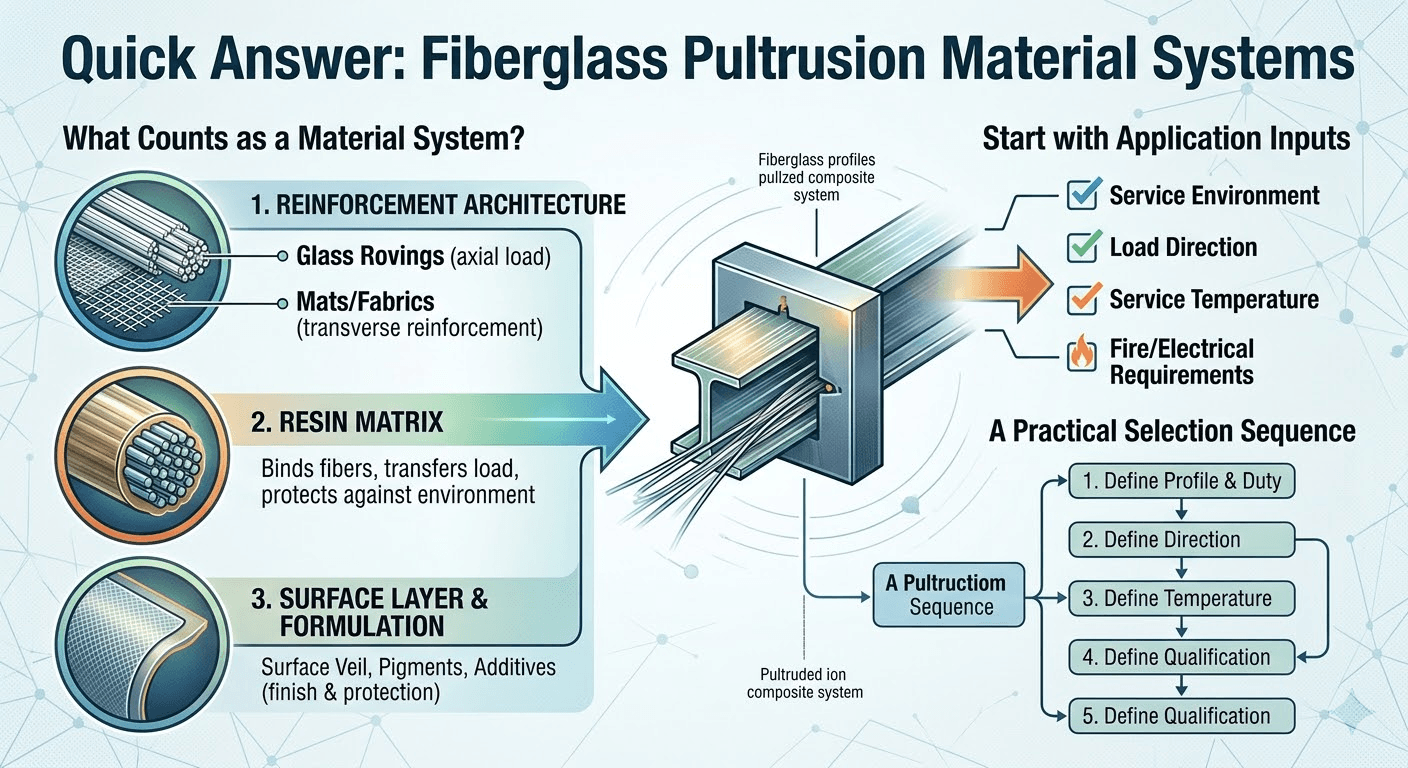
Fiberglass pultrusion materials work as a system rather than as interchangeable ingredients. Continuous glass rovings mainly support loads along the profile, mats or fabrics add reinforcement across the section, the resin binds and protects the fibers, and a surface veil modifies the outer layer. Selection should begin with load direction, service environment, temperature, fire or electrical requirements, surface expectations, geometry, and the evidence required for acceptance—not with a generic “best resin” or fiber percentage.
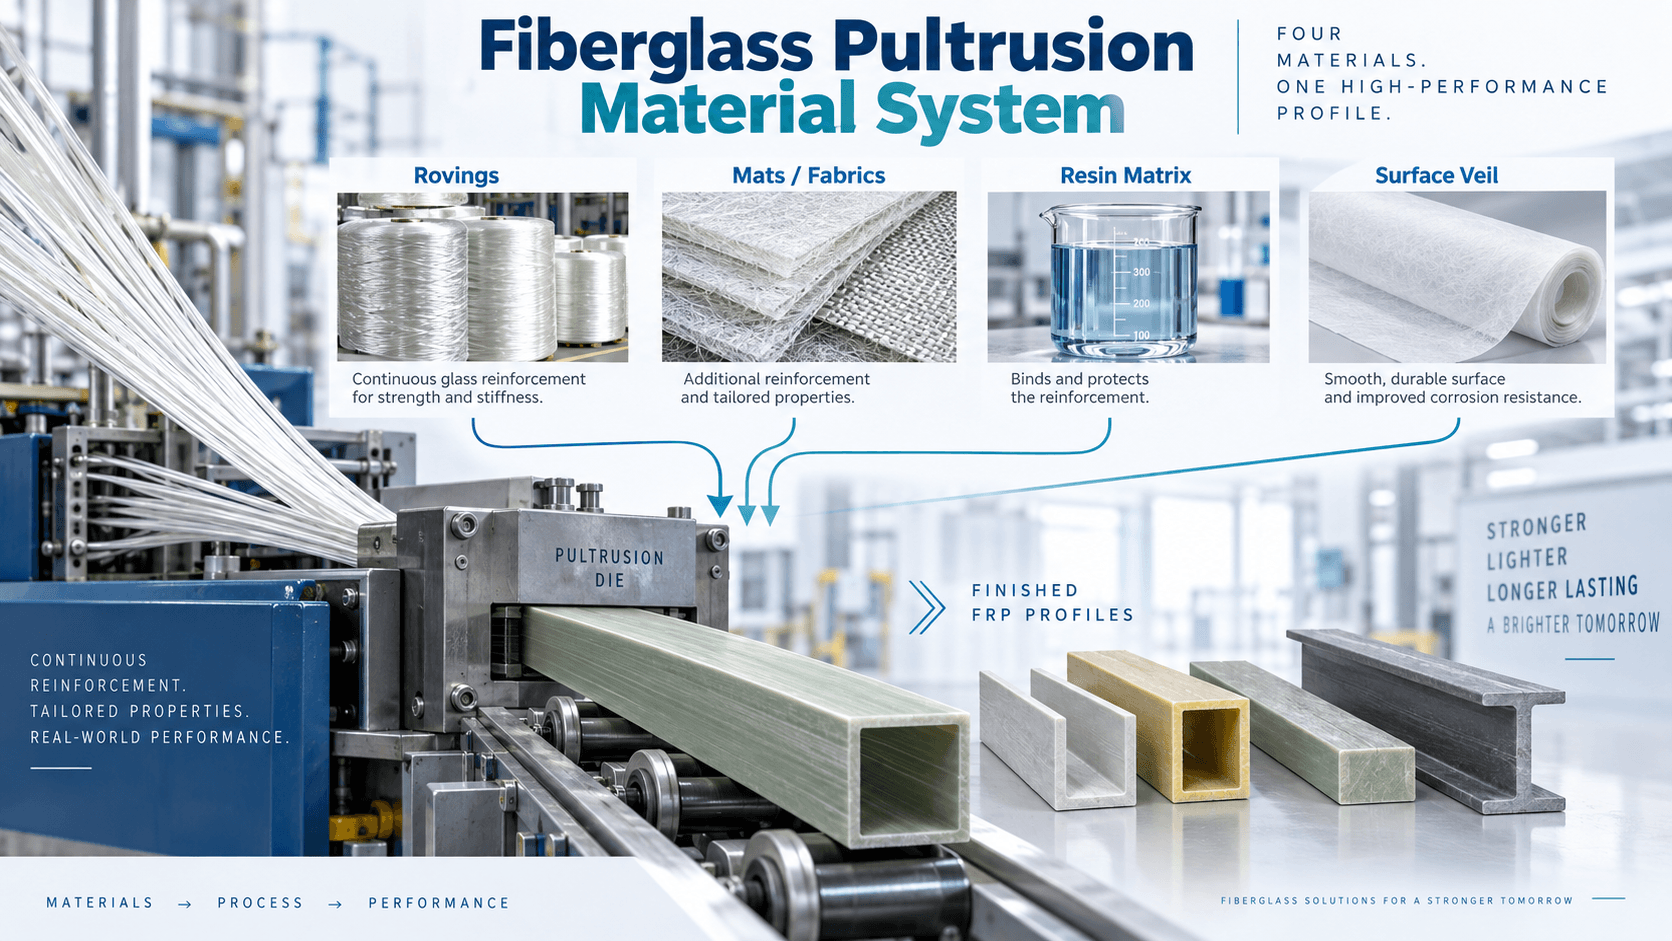
fiberglass pultrusion material system
What Counts as a Fiberglass Pultrusion Material System?
A pultruded fiberglass profile is a composite system built from three interacting parts:
- Reinforcement architecture: the type, orientation, and placement of glass rovings, mats, fabrics, or other textile forms.
- Resin matrix: the polymer system that wets the reinforcement, transfers load between fibers, supports the profile shape after cure, and contributes to environmental performance.
- Surface layer and formulation: surface veil and any project-specific pigments, fillers, processing aids, or functional additives.
The manufacturing process pulls the reinforcement through impregnation and a heated die to produce a continuous profile. This article focuses on material selection; for the complete production sequence, see Pultrusion Process: How Continuous FRP Profiles Are Made.
Research and industry sources describe pultrusion as a coupled material-and-process system. Reinforcement form, resin behavior, wet-out, fiber placement, thermal history, and profile geometry influence one another, so a material cannot be qualified reliably from its trade name alone.[1][2]
Start with Application Inputs, Not a Material Name
The most useful material brief translates service requirements into decisions about reinforcement, matrix, surface layer, and qualification evidence.
| Project input | Reinforcement question | Resin or surface question | Evidence to define before approval |
|---|---|---|---|
| Primary load direction | How much of the load is longitudinal, transverse, bearing, or localized? | Does the matrix support the required load transfer and service conditions? | Design values, test method, specimen direction, conditioning, and acceptance limit |
| Chemical exposure | Which chemicals, concentrations, temperatures, and exposure durations matter? | Which resin and surface construction are candidates for that exact exposure? | Compatibility data or project-specific testing under stated conditions |
| Service temperature | What sustained and peak temperatures occur, and under what load? | Can the cured system remain suitable over the required range? | Applicable thermal data, conditioning, and acceptance method |
| Fire and smoke requirements | Does the reinforcement arrangement affect the required section or test specimen? | Which complete formulation is to be tested—not merely which resin family is named? | Required code, test standard, specimen configuration, and pass/fail criteria |
| Electrical function | Is insulation, controlled conductivity, or another behavior required? | Which complete material system and additives must be evaluated? | Relevant electrical test method and environmental conditioning |
| Surface and weathering | Is appearance, fiber coverage, handling, coating, or outdoor exposure the priority? | Is a veil or another surface treatment needed, and what must it demonstrate? | Visual standard, exposure method, coating compatibility, or surface acceptance criteria |
| Geometry and wall structure | Where are corners, thin walls, webs, hollows, or thickness transitions located? | Can the resin wet and cure the selected reinforcement architecture in that geometry? | Cross-section drawing, reinforcement plan, trial observations, and dimensional results |
| Machining and joining | Where will holes, cuts, fasteners, or bonded joints be placed? | What edge, surface, and conditioning requirements apply? | Machining drawing, joint test method, inspection criteria, and allowable damage |
This structure prevents a common specification error: selecting a resin label first and asking the remaining materials to compensate for an incomplete application definition.
Glass-Fiber Reinforcement Forms and Their Roles
Pultrusion can use rovings together with mats, scrims, fabrics, braids, or other textile semi-finished products. The appropriate combination depends on how the profile is loaded and how reinforcement can be positioned through the section.[1]
Continuous Rovings
Continuous rovings run mainly in the pulling direction. They primarily contribute to longitudinal stiffness and tensile capacity and are therefore central to profiles carrying axial or bending loads. However, bending behavior also depends on section geometry, reinforcement distribution, matrix behavior, local stability, and shear transfer. A profile that carries loads in more than one direction cannot be assessed from roving content alone.
The specification should identify:
- the important load directions;
- the required design properties and test orientations;
- local bearing, connection, and cutout regions;
- the profile geometry that the bundles must follow; and
- the acceptance evidence required for the finished profile.
Mats, Fabrics, and Other Textile Forms
Mats, stitched fabrics, woven fabrics, scrims, and other textile forms can introduce reinforcement in directions and locations that are not provided by longitudinal rovings alone. Their contribution depends on fiber orientation, continuity, placement, and integration within the section architecture. A review of FRP structures distinguishes the longitudinal role of unidirectional rovings from the additional directional roles that mats and woven or stitched fabrics can provide.[3]
The name of a textile form does not establish finished-profile performance. Orientation, continuity, placement, wet-out, local distortion, resin compatibility, and the test direction still matter.
Why Reinforcement Architecture Matters
Two profiles made with the same broad fiber and resin families may behave differently if their reinforcement is distributed differently. Corners, thin webs, hollow regions, holes, joints, and concentrated loads can require attention beyond the nominal longitudinal properties.
For procurement, request a reinforcement description that is detailed enough to connect the proposed architecture to the drawing and acceptance tests. Avoid relying only on a single total glass-content value or a generic material label.
What the Resin Matrix Must Do
The resin matrix is not simply a filler around the glass. It must wet the reinforcement, transfer stress between fibers, hold the cured geometry, protect the reinforcement from the service environment, and remain compatible with the production window.
Pultrusion research and development commonly covers unsaturated polyester, vinyl ester, epoxy, and polyurethane systems, alongside specialized formulations.[1] These are families rather than guaranteed performance levels. Cure chemistry, additives, fiber sizing, processing conditions, final laminate construction, and test conditions can all change the result.
A Better Way to Compare Resin Systems
Instead of ranking resin families as “good, better, best,” compare candidate systems against the actual project:
- Exposure: chemicals, water, humidity, ultraviolet exposure, and cleaning agents.
- Temperature: sustained and peak values, exposure duration, and simultaneous mechanical load.
- Mechanical duty: load direction, duration, fatigue or impact concerns, and connection details.
- Regulated performance: the exact fire, smoke, electrical, or other standard that applies.
- Processing compatibility: viscosity, wet-out behavior, cure response, reinforcement permeability, and profile geometry.
- Verification: specimen construction, conditioning, test method, sampling frequency, and acceptance limit.
A resin family is a material category, not a finished-profile performance rating. A resin family name by itself does not prove chemical resistance, fire performance, electrical behavior, or service life. Those claims require evidence for the complete formulation and finished material system under defined conditions.
What a Surface Veil Does—and Does Not Prove
A surface veil is a thin outer reinforcement layer used in many pultruded constructions. Technical literature describes it as part of the surface-finish and protection strategy, while the underlying rovings and textile layers carry their own structural roles.[3]
Depending on the veil material, resin system, processing conditions, and profile construction, a surface veil may contribute to a more resin-rich outer region, better coverage of structural reinforcement near the surface, reduced visible fiber print, and a more controlled surface finish. Its intended function should be written into the project specification instead of assumed from the word “veil.”
A surface veil alone does not prove:
- resistance to a particular chemical and concentration;
- a stated outdoor service life;
- compliance with a fire or smoke requirement;
- coating adhesion;
- a specific surface-quality grade; or
- freedom from all surface defects.
Define the required surface outcome and how it will be inspected or tested. That keeps a visual feature from being mistaken for a performance guarantee.
How Materials Interact with the Pultrusion Process
Material selection and process definition cannot be separated completely. Review literature identifies resin viscosity, fiber permeability, impregnation, cure development, heat transfer, pulling behavior, and die conditions as connected parts of pultrusion.[2]
Important interactions include:
- Fiber sizing and resin compatibility: the fiber surface treatment and matrix must support wet-out and the intended interface.
- Textile permeability and impregnation: dense or complex reinforcement arrangements can change how resin reaches internal regions.
- Viscosity and temperature: flow behavior changes with temperature and formulation, affecting impregnation and process stability.
- Cure and thermal history: the profile must develop an appropriate cure through its cross-section without relying on one universal temperature or line-speed setting.
- Reinforcement placement and geometry: corners, wall transitions, hollows, and local features affect preforming, compaction, and resin distribution.
- Additives and fillers: changes intended for color, fire behavior, cost, shrinkage, or processing can also change flow and cure behavior and therefore require evaluation.
For a practical method of evaluating the coupled thermal process window, see Pultrusion Die Heating: How Temperature and Line Speed Work Together.
A Practical Material-Selection Sequence
1. Define the Finished Profile and Its Duty
Provide the cross-section drawing, critical dimensions, load directions, connection and machining details, service environment, design life assumptions, and any regulated requirements. Separate mandatory acceptance criteria from preferences.
2. Translate Requirements into Material Functions
Identify which functions must come primarily from longitudinal reinforcement, transverse or surface reinforcement, matrix behavior, surface construction, or a tested combination of these elements.
3. Screen Candidate Material Systems
Compare complete candidate constructions, not isolated resin names. Record the reinforcement forms and orientations, resin system identification, surface layer, relevant additives, and any assumptions that still require validation.
4. Check Process and Tooling Inputs
Confirm that the selected architecture can be guided, impregnated, formed, heated, and pulled through the proposed cross-section. Material decisions become tooling inputs when they affect cavity allowance, entrance geometry, preforming, mandrels or inserts, heating strategy, and expected pulling behavior.
If a project requires a new or modified die, review our pultrusion molds and tooling and include the material system in the tooling discussion.
5. Define Qualification Before Production
Agree on what evidence will approve the material system. Depending on the project, this may include supplier documentation, incoming checks, profile dimensions, visual inspection, mechanical tests by direction, environmental conditioning, fire or electrical tests, and traceable change control.
Do not leave the test method, specimen condition, sample location, or acceptance limit until after the first production run.
fiberglass pultrusion materials
Material Qualification and Procurement Checklist
Use the following checklist to prepare a material-system review:
- Profile drawing and revision
- Critical dimensions and tolerances
- Primary, transverse, bearing, and localized load cases
- Required design properties and test directions
- Chemical names, concentrations, temperatures, and exposure modes
- Sustained and peak service temperatures
- Outdoor, ultraviolet, moisture, or immersion conditions
- Applicable fire, smoke, electrical, or other regulated tests
- Surface appearance, handling, coating, and inspection requirements
- Machining, drilling, fastening, and bonding details
- Candidate reinforcement forms and placement assumptions
- Candidate resin system and formulation identification
- Surface veil or other outer-layer requirement
- Required material documents and incoming checks
- Prototype or trial requirements
- Finished-profile test methods, conditioning, sampling, and acceptance limits
- Change-notification and requalification rules
Common Material-Selection Mistakes
Treating a Resin Family as a Performance Specification
“Vinyl ester,” “polyester,” or “epoxy” is not a complete acceptance requirement. State the service condition and the evidence the finished material system must meet.
Specifying Only Longitudinal Strength
Pultrusion naturally favors continuous reinforcement in the pulling direction, but real profiles also contain corners, joints, holes, webs, and loads outside that direction. Define the other relevant directions and local conditions.
Assuming a Veil Guarantees Durability
A veil can contribute to the surface construction. It does not replace chemical-compatibility evaluation, weathering evidence, coating qualification, or inspection criteria.
Copying a Generic Fiber Percentage
A total fiber value does not describe fiber form, orientation, placement, local continuity, or voids. Link the proposed architecture to the profile drawing and test evidence.
Changing Formulation Without Reviewing the Process Window
Resin, catalyst, filler, pigment, release agent, fiber sizing, or textile changes may affect wet-out, cure, heat transfer, pulling behavior, and finished properties. Define which changes require approval or requalification.
Related Pultrusion Resources
- Pultrusion Process: How Continuous FRP Profiles Are Made — the full manufacturing sequence and process controls.
- Pultrusion Die Heating: How Temperature and Line Speed Work Together — a process-window method for heating, cure, and line speed.
- FRP Pultrusion Process: Advantages and Disadvantages — when constant-section pultrusion fits an application and where its limits matter.
Prepare a Better Material and Tooling Discussion
There is no universal fiberglass pultrusion material package for every profile. A defensible selection connects reinforcement architecture, resin behavior, surface construction, geometry, process conditions, and acceptance evidence to one defined application.
Send us your profile drawing, critical tolerances, load and environment inputs, proposed reinforcement and resin information, target production conditions, and acceptance requirements. We can use that information to define the quotation scope and identify the tooling and documentation requirements that still need to be addressed.
References
- Fraunhofer Institute for Casting, Composite and Processing Technology IGCV, Pultrusion: Processing Know-How for Resin Systems, Fibers and Textiles.
- Volk, M., Yuksel, O., Baran, I., Hattel, J. H., Spangenberg, J., and Sandberg, M., Cost-efficient, automated, and sustainable composite profile manufacture: A review of the state of the art, innovations, and future of pultrusion technologies, Composites Part B: Engineering, 246 (2022), 110135.
- Qureshi, J., A Review of Fibre Reinforced Polymer Structures, Fibers, 10(3) (2022), 27.


